Industry Solutions
Industry Solutions
Covering six industry groups and 36 application scenarios, matching industrial wastewater treatment, reuse, reduction, and resource-recovery goals with practical engineering routes.
Locate scenarios by industry
Identify comparable applications
Move from application to engineering route
Industrial Sectors
Six Industry Groups and 36 Application Scenarios
Select an industry group to identify comparable process streams; scenarios with details can be opened by clicking the image.
Chemical & Petrochemical
For waste acids, high-salinity mother liquors, refinery wastewater, and fermentation purification, assess segregated recovery, desalination, concentration, and resource recovery.
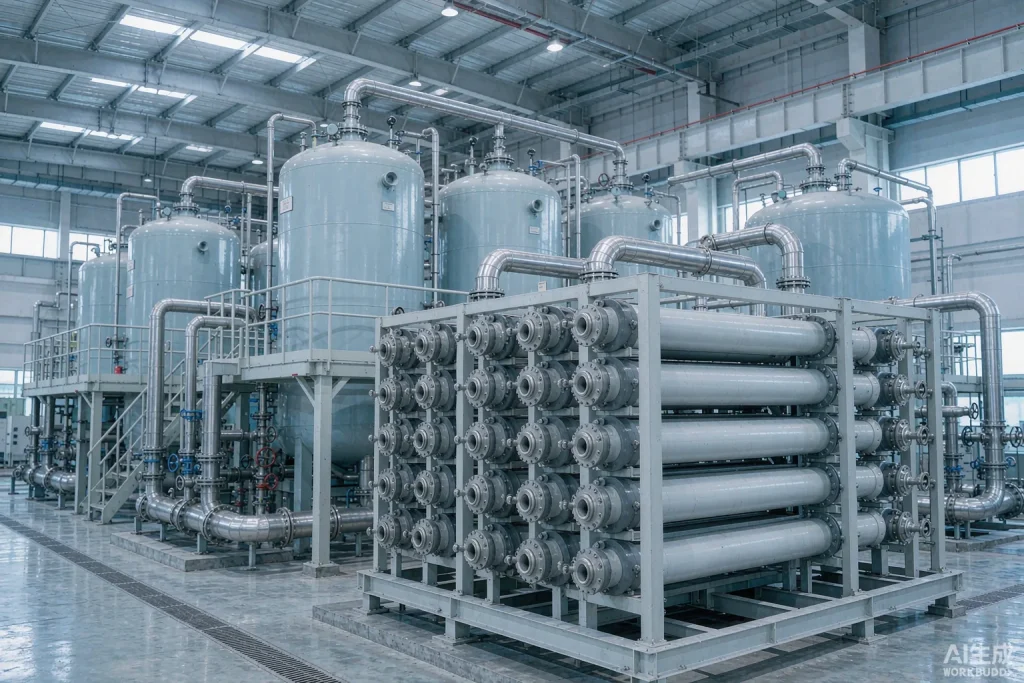
Waste-acid recovery for titanium dioxide, fluorochemicals, pesticides, and dyes
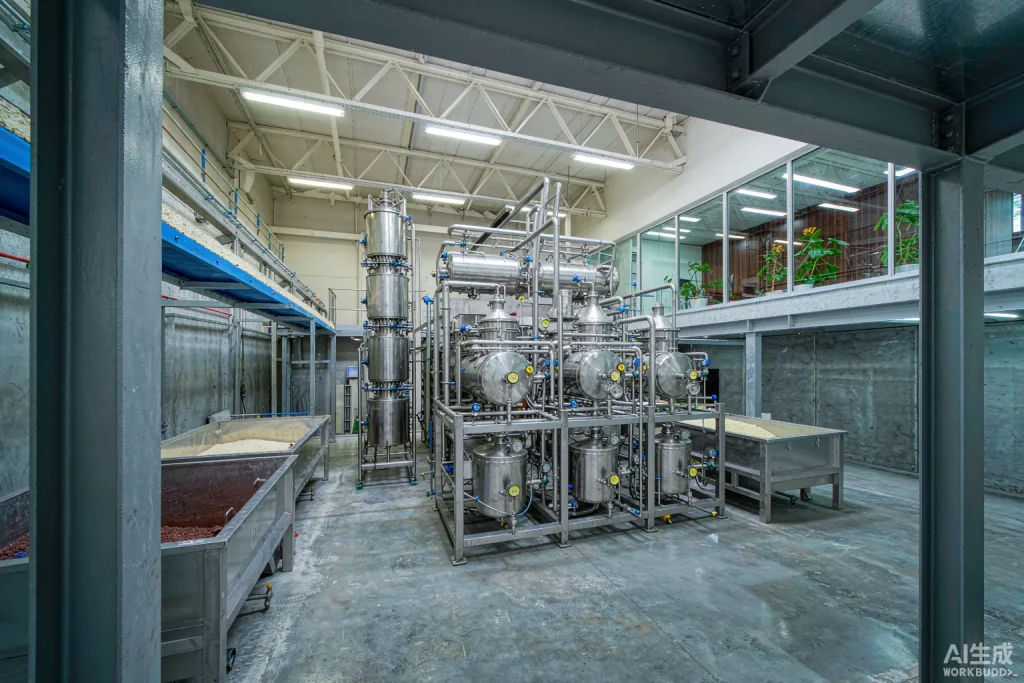
Acidic waste-liquor recovery from wood hydrolysis
Recovery and regeneration of acidic pharmaceutical mother liquor
Closed-loop acid reuse in paper production
Concentration of sodium chloride, sodium sulfate, and ammonium chloride
Resource recovery from inorganic salts and process mother liquors
High-salinity wastewater reduction in coal chemical processing
Preconcentration upstream of MVR evaporation
Desalination of integrated refinery wastewater
Desalination of amino-acid, citric-acid, lactic-acid, and glutamic-acid fermentation broths
Purification and refining of fermentation broth
Desalination and refining of active pharmaceutical ingredients
Purification of pharmaceutical intermediates
Purification of fermentation-derived pharmaceuticals
Recovery of lactic, citric, and gluconic acids
Recovery of itaconic, succinic, and acetic acids
Nonferrous Metals & Rare Earths
Across nonferrous-metal pickling, hydrometallurgy, and rare-earth salt systems, identify opportunities for acid regeneration, metal-salt conversion, and valuable-component recovery.
Spent-acid recovery from copper, aluminum, and titanium pickling
Waste-acid treatment in copper, nickel, zinc, and cobalt smelting
Acid recovery in the Bayer process
Recovery and regeneration of hydrochloric and nitric acids in rare-earth processing
Rare-earth salt conversion
Conversion of nickel, cobalt, and copper salts
Electroplating & Surface Treatment
For electroplating, PCB, formed-foil, and electronic-chemical processes, recover acids and support closed-loop production of high-purity acids and alkalis.
Recovery and regeneration of hydrochloric, sulfuric, and nitric acids
Spent-acid recovery from micro-etching and etching
Spent-acid recovery from foil-forming processes
Production of high-purity electronic-grade acid
Production of high-purity electronic-grade alkali
New Energy & Lithium Batteries
Covering cathode materials, lead-acid batteries, lithium-salt conversion, salt-lake lithium extraction, and precursor production, with emphasis on separating and converting lithium and metal salts.
Treatment of acid-leach waste liquor from cathode materials
Spent-acid recovery from lead-acid battery production
Lithium-salt conversion from lithium sulfate to lithium hydroxide
Lithium extraction from salt-lake brines
Metal-salt conversion for power-battery cathode materials
Production of ternary precursors and lithium iron phosphate
Textile & Dyeing
Focus on recovering and reusing free acid from fabric-pickling waste liquor to reduce neutralization chemicals, salt load, and liquid waste.
Recovery of spent acid from fabric pickling
Steel & Coking
For hydrochloric- and sulfuric-acid steel pickling, recover free acid and segregate iron-rich side streams to reduce fresh-acid use and neutralization load.
Recovery of spent hydrochloric-acid pickling liquor
Recovery of spent sulfuric-acid pickling liquor
Convert Water quality reports into executable process routes
Submit water quality, flow rate, target products, and site boundary conditions. EasyGu Water Treatment engineers can develop preliminary solutions for industrial wastewater treatment, water reuse, zero liquid discharge (ZLD), and resource recovery objectives.

Project Inquiry
Tell us your water quality and objectives
Submit the currently available industry, water volume, main components, existing process, and objectives. Incomplete information can also be submitted first, and engineers will assist in supplementing the boundary conditions later.
- Phone400-022-8199 / 0551-63618199
- Business Email[email protected]
- Service HoursMon-Fri 8:30-17:30
Project & Partnership Inquiry
Select an inquiry type and share the information available. Our engineers will follow up with the source page context.